|
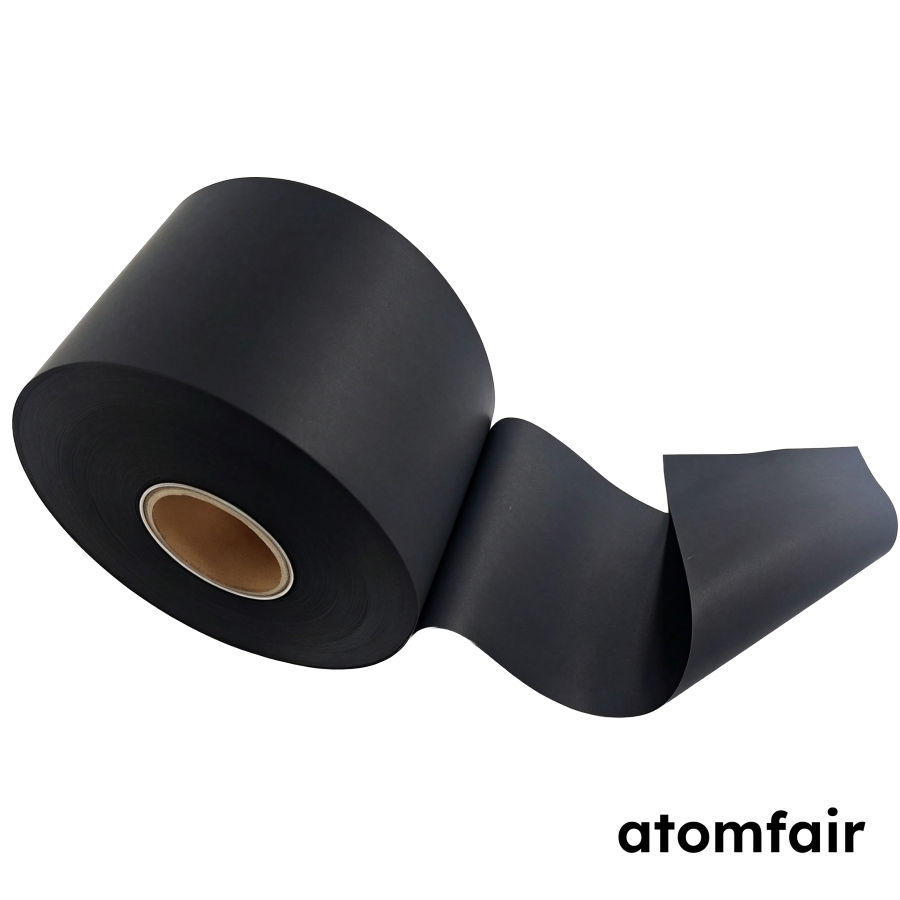
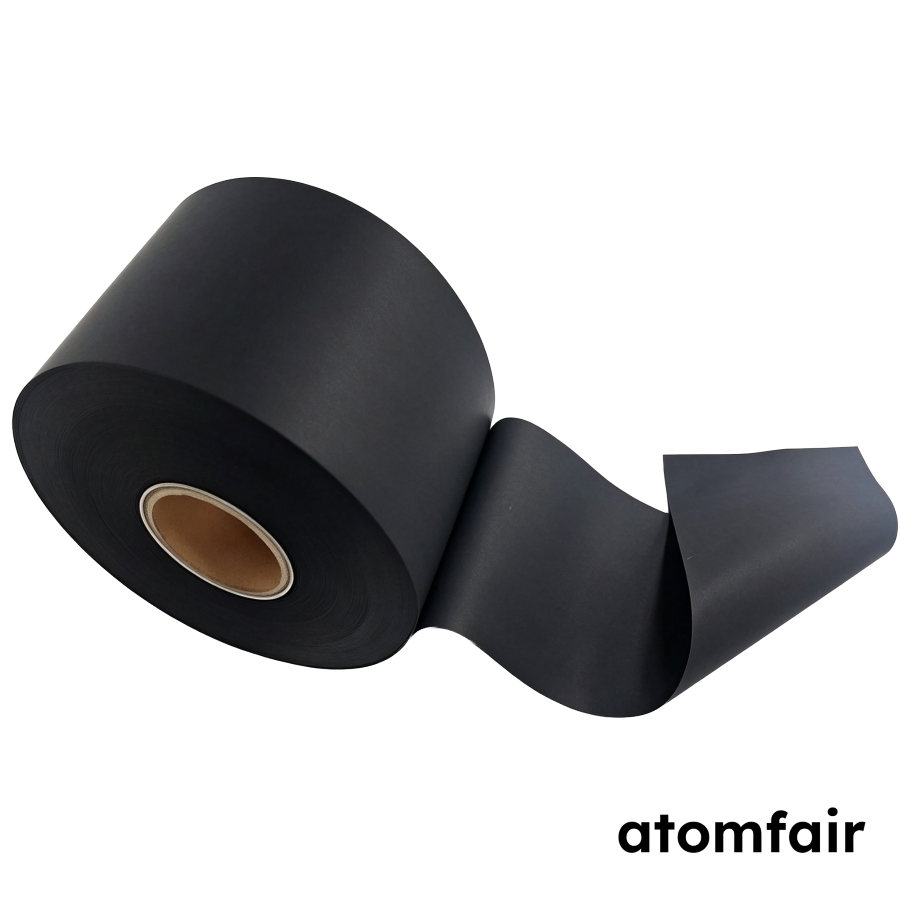
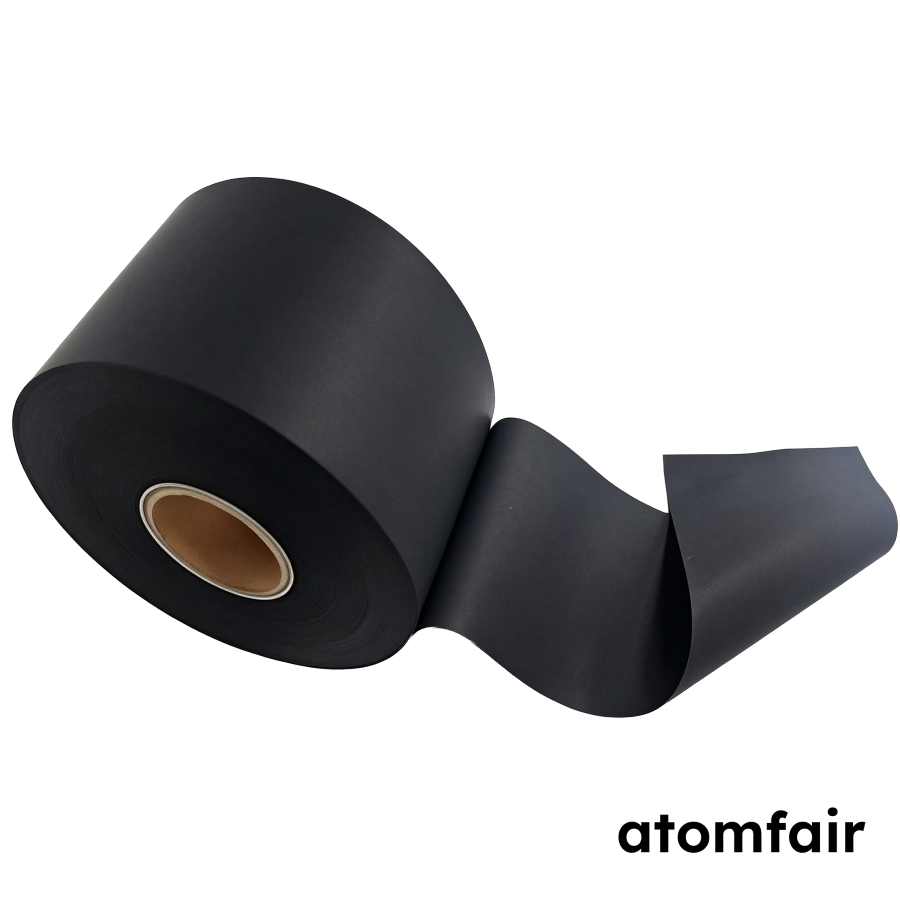
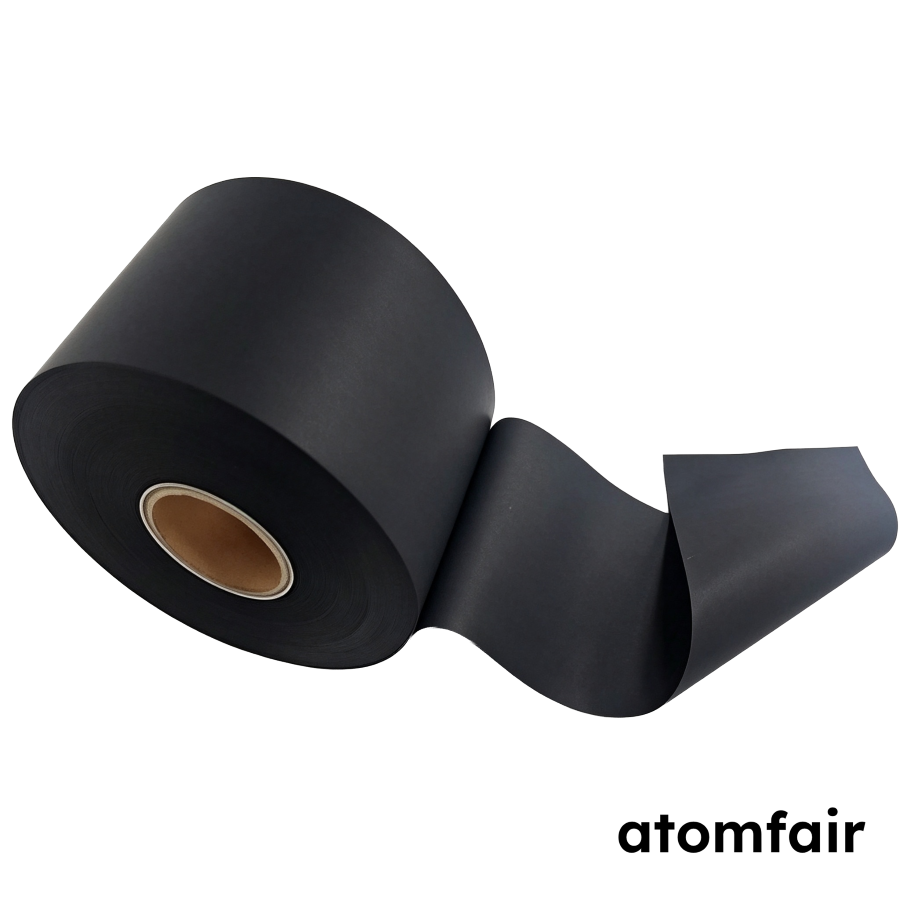
PTFE-Bonded Acetylene Black Electrode Sheet for Primary Batteries, 200 μm
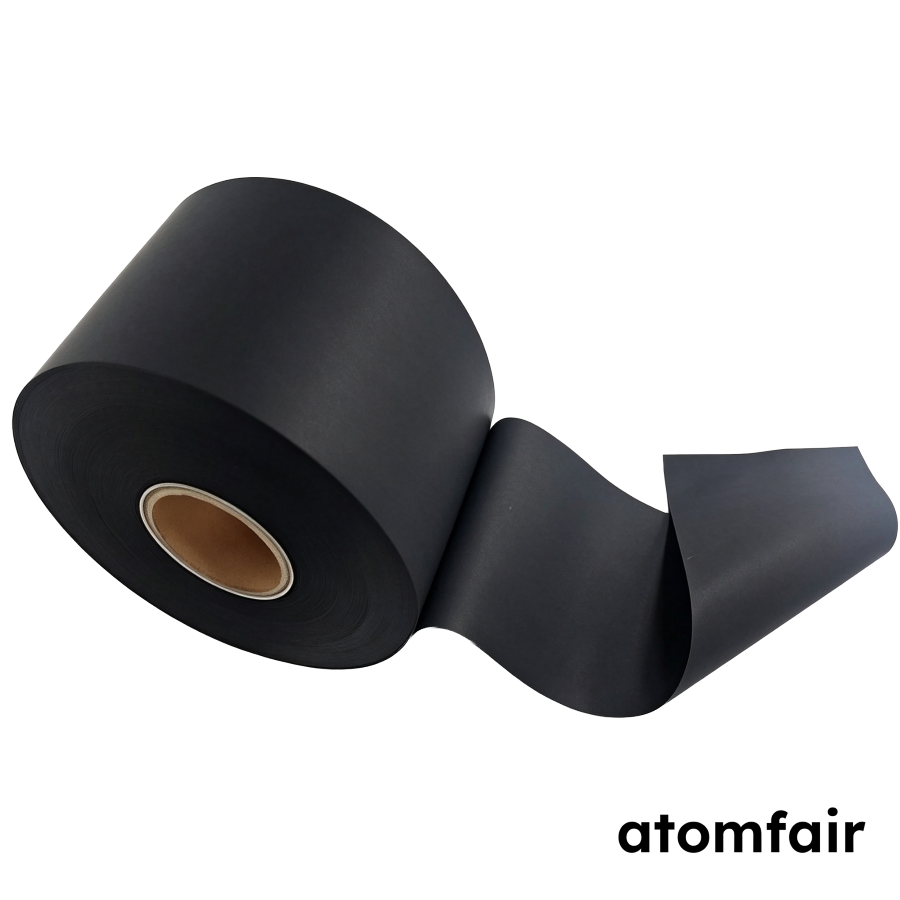
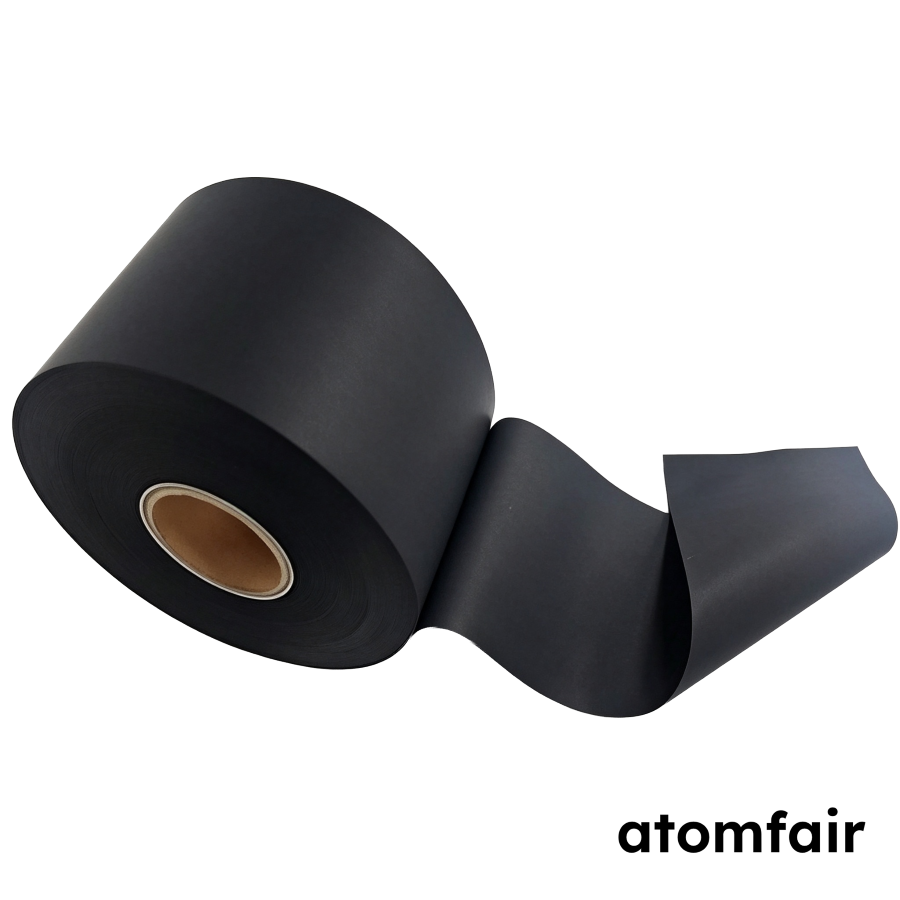
PTFE-Bonded Roll-Form Carbon Electrode Sheet
|
||||||||||||||||||||||||||||||||||||||||||||||||||||||
|
This carbon electrode sheet requires controlled drying at 90–100°C for 12–24 hours prior to cell assembly to remove residual moisture. The sheet must be handled in a clean, dry environment to avoid bending, scratching, or contamination that could compromise electrode performance.
- Drying Requirement: Dry the electrode sheet at 90–100°C for 12–24 hours before cell assembly to eliminate adsorbed moisture.
- Handling Environment: After drying, transfer the sheet to a clean, dry environment and avoid exposure to ambient humidity.
- Mechanical Integrity: Maintain tensile strength above 5 N by preventing bending, scratching, or creasing during cutting and transfer.
- Downstream Lamination Compatibility: The sheet is designed for downstream current-collector lamination workflows in primary battery research.
- Contamination Sensitivity: Avoid contaminating the coated surface with oils, particulates, or moisture during electrode preparation.
This procedure outlines the drying and handling steps required to prepare the roll-form carbon electrode sheet for primary battery cell assembly. Proper execution ensures the sheet maintains its mechanical integrity and electrochemical performance.
Required Equipment: Drying oven, Clean handling environment
- Dry the electrode sheet
Dry the electrode sheet in an oven at 90–100°C for 12–24 hours to remove residual moisture before cell assembly. - Transfer to clean environment
Transfer the dried sheet to a clean, dry handling environment immediately after drying to prevent moisture reabsorption. - Cut or punch without damage
Cut or punch the sheet to the desired dimensions while avoiding bending, scratching, or contaminating the coated surface.
How does the PTFE binder content (from 5%) affect the mechanical and electrical properties of this acetylene black electrode sheet?
The PTFE binder at a minimum of 5% provides the necessary mechanical integrity to form a flexible roll-form sheet with a tensile strength >5 N, enabling handling and downstream processing. The low binder content allows the acetylene black content to reach up to 95%, preserving the high conductivity of the carbon phase for primary battery research applications.
Can this PTFE-bonded acetylene black electrode sheet be used directly in Li-SOCl2 cell assembly without a current collector?
This sheet is intended for primary battery research including Li-SOCl2, but it is supplied as a preformed carbon electrode layer that requires lamination onto a current collector as part of downstream electrode preparation. The description explicitly references 'downstream current-collector lamination workflows,' so the sheet is not a standalone electrode with an integrated current collector.
What are the critical drying and handling procedures for this 200 µm acetylene black electrode sheet to ensure reproducible performance?
The sheet must be dried at 90–100°C for 12–24 hours prior to cell assembly to remove adsorbed moisture. After drying, handle the sheet in a clean, dry environment and avoid bending, scratching, or contaminating the coated surface during cutting, punching, transfer, and stacking, as mechanical damage or contamination can compromise electrode uniformity and performance.
Preformed acetylene black/PTFE electrode sheet at 200 µm thickness with areal density 7.0 mg/cm² and compaction density 0.35 g/cm³, supplied in roll form with customizable width for primary battery research (e.g., Li-SOCl2). Requires drying prior to assembly and careful handling.
Positive
- Ready-to-use roll-form sheet: Supplied as a preformed, PTFE-bonded acetylene black sheet in roll form, eliminating the need for in-house powder processing and enabling direct integration into laboratory cell assembly workflows.
- Customizable width with tight tolerance: Width adjustable from 50-300 mm with ±0.3 mm control, allowing precise fitting to specific cell geometries or current-collector substrates without additional trimming overhead.
Trade-offs
- Required drying step before use: The electrode sheet must be dried at 90-100°C for 12-24 hours prior to cell assembly, adding a preprocessing step and requiring oven capacity with stable temperature control.
- Handling sensitivity after drying: Post-drying, the sheet is vulnerable to bending, scratching, and contamination, necessitating a clean and meticulous handling environment during cutting, punching, and stacking.
Every advanced material, component, equipment, and instrument in our catalog is backed by rigorous testing. We maintain strict internal quality management frameworks and align with CE conformity metrics to deliver transparent, reproducible performance data via our public open-science repository.
To request raw batch performance data, submit formal vendor registration paperwork, or execute a fast-turnaround R&D manufacturing loop, contact us at inquiry@atomfair.com.
Item is dispatched under the Atomfair Shipping & Delivery Framework (Free worldwide shipping on orders over $59 USD excl. heavy equipment). Return is governed by the Atomfair Return & Refund Policy (7-day technical return window).