|
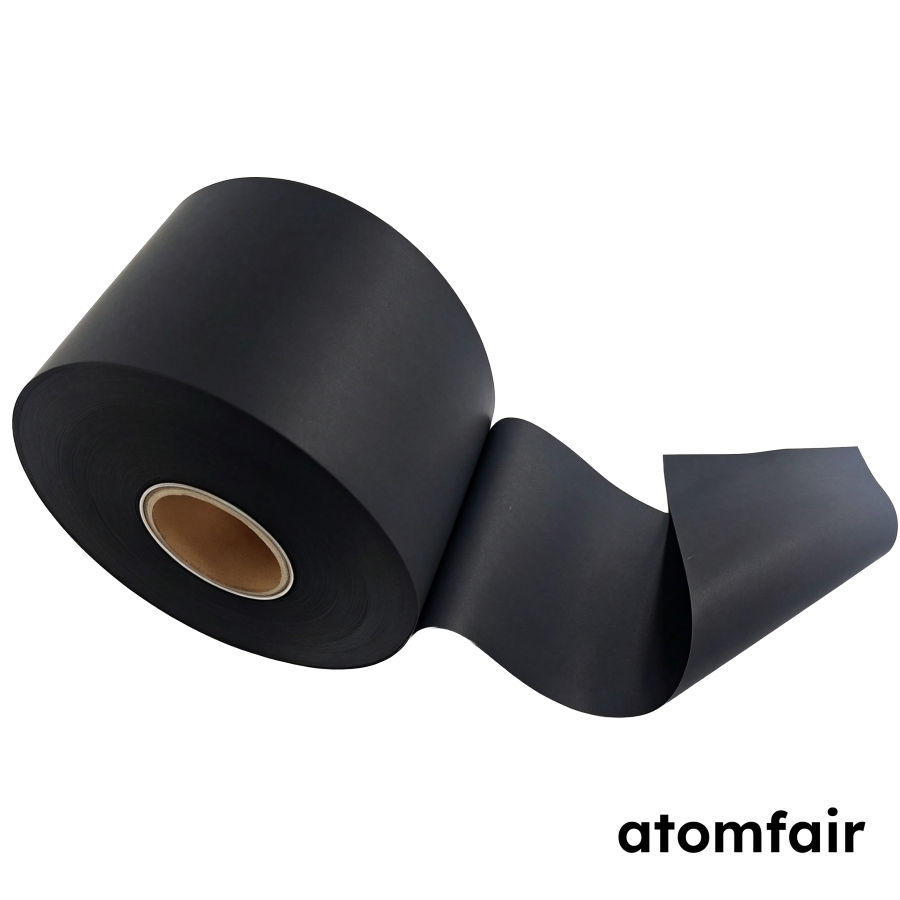
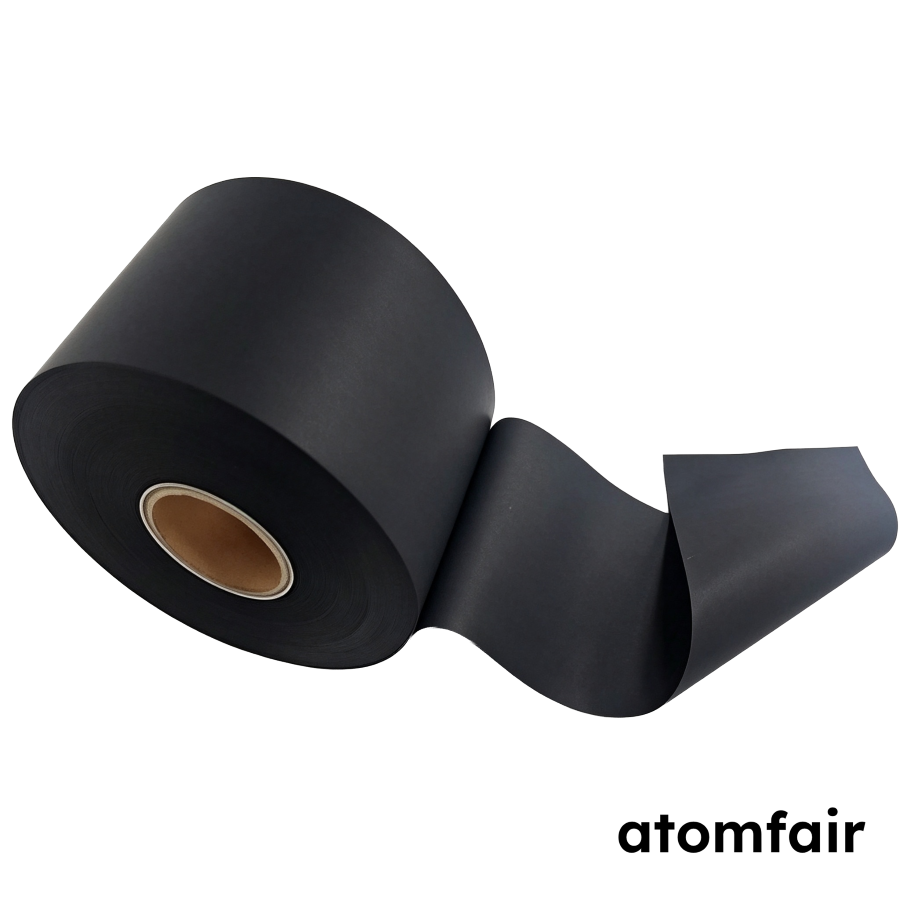
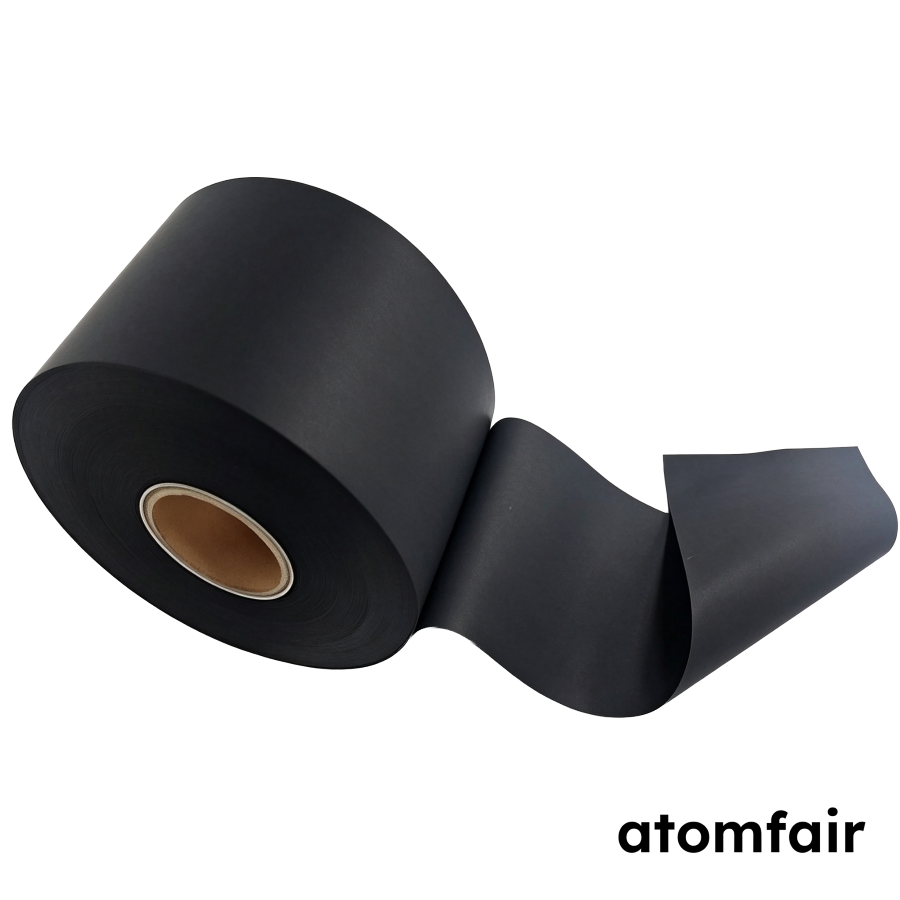
PTFE-Bonded Acetylene Black Electrode Sheet for Primary Batteries, 700 μm
PTFE-Bonded Roll-Form Carbon Electrode Sheet
|
||||||||||||||||||||||||||||||||||||||||||||||||||||||
|
The electrode sheet requires drying at 90-100°C for 12-24 hours prior to cell assembly to remove adsorbed moisture. After drying, the sheet must be handled in a clean, dry environment and protected from bending, scratching, or contamination during downstream processing.
- Drying Requirement: Dry the electrode sheet at 90-100°C for 12-24 hours before cell assembly to remove adsorbed moisture.
- Handling Environment: After drying, handle the sheet only in a clean, dry environment to prevent moisture reabsorption and contamination.
- Mechanical Precautions: Avoid bending, scratching, or contaminating the coated surface during cutting, punching, transfer, and stacking.
- Tensile Strength Constraint: The sheet's tensile strength exceeds 5 N, requiring careful handling to avoid tearing or permanent deformation.
- Binder Thermal Stability: Maintain drying temperature within the specified range to prevent thermal degradation of the PTFE binder.
This procedure describes the required drying and handling steps for the PTFE-bonded carbon electrode sheet prior to cell assembly. Proper execution ensures electrode integrity and prevents contamination or mechanical damage.
Required Equipment: Drying oven capable of maintaining 90-100°C, Clean, dry handling environment (e.g., glovebox or dry room), Cutting tool (sharp blade or precision punch)
- Dry the electrode sheet
Dry the electrode sheet at 90-100°C for 12-24 hours in a ventilated oven to remove adsorbed moisture. - Transfer to clean environment
Transfer the dried sheet to a clean, dry handling environment such as a glovebox or dry room immediately after drying. - Cut to desired dimensions
Cut the sheet to the required dimensions using a sharp blade or precision punch, avoiding bending or scratching the coated surface. - Transfer cut pieces
Transfer the cut electrode pieces to the cell assembly station using clean tweezers or a vacuum pickup tool to avoid contamination. - Stack with other components
Stack the electrode pieces with separator and other cell components as per the cell design, ensuring no contamination or misalignment.
How does the compaction density of 0.33 g/cm³ affect the electrode porosity and electrochemical performance in Li-SOCl₂ primary batteries?
The compaction density of 0.33 ± 0.01 g/cm³ is a key physical parameter that influences porosity, but it must be interpreted alongside loading, thickness, and the source measurement method. The source states that this parameter, combined with the areal density of 23.1 ± 0.5 mg/cm², defines the electrode's structural properties. Researchers should evaluate porosity relative to the electrolyte system and intended discharge rate.
Can this acetylene black-based electrode sheet be directly laminated onto a nickel or stainless steel current collector, and what adhesive or pressure is required?
The sheet is designed for downstream current-collector lamination workflows, as indicated in the product description under typical research uses. However, the source does not specify a particular adhesive, pressure, or temperature for lamination. The flexible roll-form with tensile strength >5 N allows mechanical handling, but users should contact the manufacturer for specific lamination parameters compatible with the PTFE binder.
What are the exact drying conditions and handling precautions to prevent delamination or contamination of the 700 µm electrode sheet?
Dry the electrode sheet at 90-100 °C for 12-24 hours before cell assembly, as specified in the product description. After drying, handle in a clean, dry environment and avoid bending, scratching, or contaminating the coated surface during cutting, punching, transfer, and stacking. The tensile strength >5 N ensures mechanical integrity during these steps.
This 700 µm preformed acetylene black/PTFE roll electrode sheet provides customizable width (±0.3 mm tolerance) and consistent areal density for primary battery research, including Li-SOCl2 systems. Its low tensile strength (>5 N) necessitates careful drying at 90–100°C for 12–24 hours and delicate handling to avoid damage.
Positive
- Preformed roll eliminates powder handling: Supplied as a ready-to-use, PTFE-bonded sheet instead of loose acetylene black powder, enabling direct lamination to current collectors and reducing laboratory powder handling complexity.
- Customizable width with tight tolerance: Width adjustable from 50–300 mm with ±0.3 mm control, allowing tailored electrode dimensions for various primary battery cell geometries without post-processing.
Trade-offs
- Mandatory extended drying protocol: Requires drying at 90–100°C for 12–24 hours prior to cell assembly, adding significant preparation time and oven capacity demands.
- Low tensile strength requires careful handling: With a tensile strength of only >5 N, the sheet is prone to tearing if bent, scratched, or contaminated during cutting, punching, or stacking.
Every advanced material, component, equipment, and instrument in our catalog is backed by rigorous testing. We maintain strict internal quality management frameworks and align with CE conformity metrics to deliver transparent, reproducible performance data via our public open-science repository.
To request raw batch performance data, submit formal vendor registration paperwork, or execute a fast-turnaround R&D manufacturing loop, contact us at inquiry@atomfair.com.
Item is dispatched under the Atomfair Shipping & Delivery Framework (Free worldwide shipping on orders over $59 USD excl. heavy equipment). Return is governed by the Atomfair Return & Refund Policy (7-day technical return window).